Bright stock
(late stage customization)
In the pharmaceutical industry, a rapid response to market needs and full flexibility in supply are essential. Collaborating using the bright stock model allows for the optimization of logistics processes, minimization of risks and costs, and, at the same time, significantly accelerates the time-to-market for products.
Benefits for manufacturers
By utilizing the bright stock model, pharmaceutical companies can:
- Optimize production costs – a single product batch can be utilized for multiple markets.
- React quickly to regulatory changes – it is sufficient to add the appropriate secondary packaging with the correct language and information.
- Minimize the risk of losses related to expiration or changes in documentation.
How the service works at Prespack
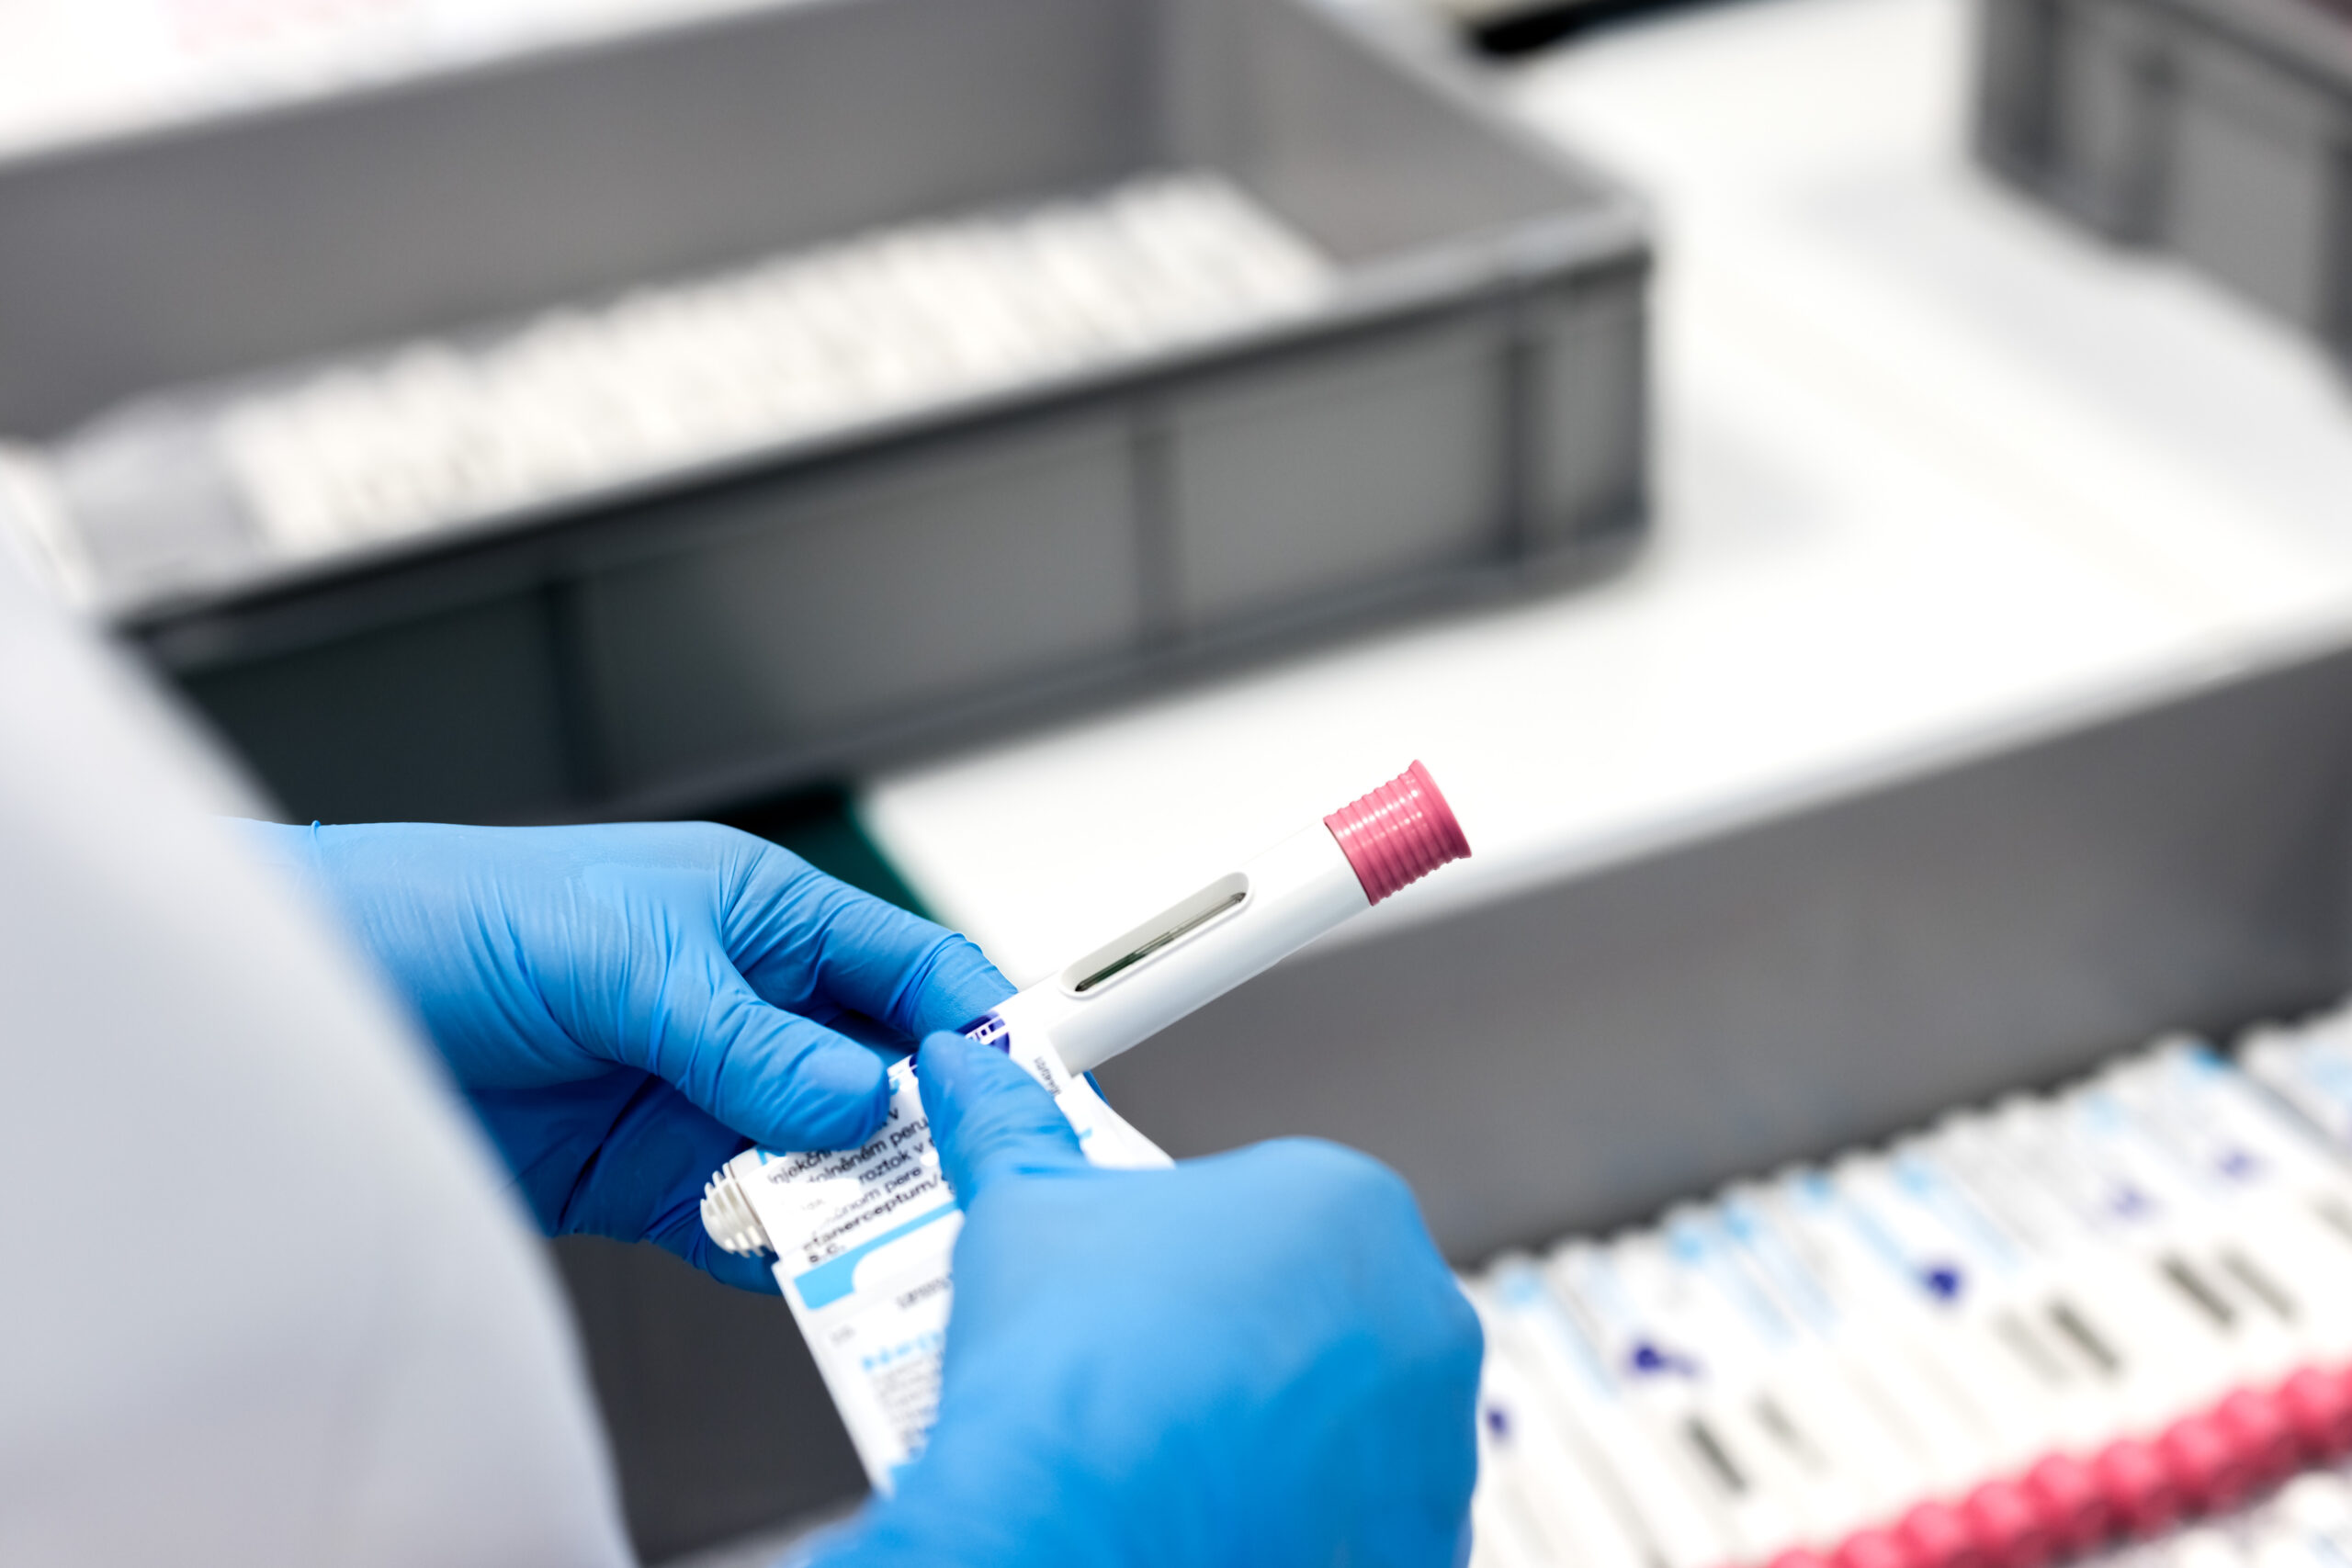
In practice, we implement the bright stock model as part of our secondary contract packaging services:
- We receive products from the client in bright stock form.
- We assemble the packaging components required for the target market (cartons, leaflets, labels).
- We package the medicinal products or kits and prepare them for distribution in full compliance with all legal and quality requirements.
Late-Stage Customization – personalization just before distribution
Increasing regulatory requirements and dynamic market changes make late-stage product customization essential. Late-stage customization allows you to:
- Adapt packaging, labels, and product kits to the specific requirements of local markets.
- Reduce costs and the risk of losses by eliminating the need to create separate batches for each market in advance.
- Maintain full compliance with drug serialization and aggregation regulations, which are necessary for safe export and distribution.
Why Choose Us
By partnering with Prespack, manufacturers can focus on the production and development of their medicines, while we take care of efficient, timely, and compliant packaging preparation. Your product, ready for every market.
Temperature-controlled storage
Prespack provides storage for products at controlled temperatures between +15°C and +25°C, as well as within the cold chain range (+2°C to +8°C). Our refrigerated chamber, with a capacity of 300 pallets, is equipped with a dual cooling system, power failure protection, and continuous temperature monitoring, ensuring the safety and full control of your products. We have plans to double our storage capacity, which will further increase our flexibility in serving our clients.
In-house printing facilities
By maintaining our own in-house printing facilities, we eliminate the risk of production downtime and optimize material logistics.
Preston Packaging is a printing house specializing in the production of packaging and leaflets for the following industries:
- pharmaceutical
- dietary supplements
- cosmetic
Our printing capabilities include:
- In-house packaging material printing: Unit cartons, PIL/IFU leaflets, inserts, and inlays.
- Modern machinery park: Heidelberg and Bobst equipment, along with advanced print inspection systems.
- Quality certifications: ISO 9001, ISO 14001, and FSC®.
- Packaging consultancy: Material selection and production preparation, including artwork revisions.
- In-house DTP studio: Preparation and consultation regarding artworks, keylines, and packaging mock-ups.
- Active inventory management: Handling packaging materials according to customer forecasts.
Discover our philosophy
of cooperation